
4. Reading the Data: What the Bubble Point Actually Tells You
1. A Representative Data Set
The table below shows typical bubble point data for a batch of sintered 316L stainless elements tested with IPA at 20 °C:
| Nominal grade | Theoretical BP for ideal round pores (kPa) | Typical measured first-bubble point (kPa / psi) | Converted largest pore neck (μm) | Share of nominal grade |
|---|---|---|---|---|
| 5 μm | 17.4 | 43 / 6.2 | ≈2.0 | ~40% |
| 10 μm | 8.7 | 22 / 3.2 | ≈3.9 | ~39% |
| 20 μm | 4.3 | 11 / 1.6 | ≈7.9 | ~40% |
| 40 μm | 2.2 | 5.5 / 0.8 | ≈15.8 | ~40% |
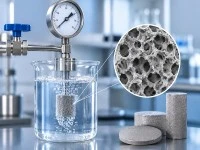
The data reveal a key fact: measured bubble points typically run 2–2.5× the theoretical value. Sintered pores are not round, straight capillaries but tortuous channels with narrow necks; the neck where gas first breaks through is usually only about 40% of the nominal pore diameter. The converted figure is therefore a largest equivalent pore neck - coming in below the nominal grade is exactly what a good element should do. A "5 μm" element whose single largest pore measures about 2 μm will reliably retain 5 μm particles.
2. Bubble Point ≠ Mean Pore Size: Three Characteristic Values

First bubble point - where the wet curve lifts off; corresponds to the largest through-pore neck and sets the floor for absolute rating;
Mean flow pore size (MFPS) - the median pore size at the dry/half-wet intersection; represents the element's overall average;
Bubble cluster point - the pressure range where bubbles emerge en masse, reflecting the population of large pores.
Only the three together describe an element completely: the bubble point guards the worst case, the MFPS guards the average. Either one alone is a half-truth.
5. Accuracy and Limitations: Six Factors That Move the Reading
Degree of wetting (largest effect): trapped air lets gas break through early, reading low and overstating pore size. Countermeasure: soak ≥10 min in IPA or vacuum-soak; start only once the element looks uniformly dark and "sinks";
Liquid temperature: IPA surface tension falls about 0.35% per °C, dragging the reading with it. Keep 20 ± 2 °C;
Pressurization rate: a fast ramp overstates the reading by 5–10% due to transmission lag. Use steps of 2 kPa held ~15 s, or ≤0.5 kPa/s;
Sealing and bypass leaks: a failed O-ring lets gas escape at the fitting and produces a fake bubble point. Check by pressurizing a blanked fitting with no element - bubbles mean a system leak;
Pore geometry: Young–Laplace assumes round, straight capillaries; sintered pores are tortuous, so treat the converted value as an "equivalent neck" and manage batch-to-batch variation (±10–15% from powder grading and sintering schedule) statistically;
Liquid contamination: water pick-up raises IPA surface tension (21.7 → ~27 mN/m at 20% water), reading high. Replace the bath regularly (every ~40 h or when cloudy).
📌 Bottom line:
under controlled conditions the test repeats within ±3%, but it measures only the largest pore - not the mean size and not the distribution. Those require the MFPS curve, mercury porosimetry or permeametry.
6. Acceptance Practice: Judging Pore Size from Bubble Point Data
1. Ask the Supplier for Three Things
The specified bubble point for that grade (minimum acceptable value, in kPa or mbar);
A test-condition statement: wetting liquid, temperature, pressurization method, and the governing standard (ISO 2942 / ASTM F316 / house standard);
Batch test records - actual per-batch data, not a "typical value" brochure page.
2. Acceptance Decision Flow
| Step | Action | Decision |
|---|---|---|
| ① Match conditions | Confirm your liquid and temperature match the supplier's statement | If not, retest before comparing - raw numbers are meaningless |
| ② Measure first bubble | Run the 6-step sequence; sample ≥3 elements per batch | Record ΔP and the converted neck size |
| ③ Compare | Measured BP ≥ specified BP × 0.95 | Accept - release the batch |
| Specified BP × 0.85 ≤ measured < ×0.95 | Retest - re-wet and test two more elements; judge on the mean | |
| Measured < specified BP × 0.85 | Reject - largest pore out of tolerance; request 100% screening or a new batch |
3. Quick Field Checks (Without a Test Bench)
Pressure-decay check: pressurize the element to 80% of the specified bubble point, shut off the supply and hold 1 min; a pressure drop under 2% indicates no significant through-pore - good for arrival screening;
Hot-water bubble check: without IPA, wet with ~60 °C water and observe as above (convert using water's surface tension at that temperature); less precise, but catches gross outliers;
Side-by-side comparison: keep one known-good element as a reference; a difference above 15% between the two on the same bench justifies a quality claim.
7. Closing Note
The value of the bubble point test is that it turns "pore size" - an invisible geometric quantity - into a pressure number that can be read in minutes and understood anywhere in the world. Grasp its three essentials - it measures the largest pore neck, it depends on wetting and technique, and it must be compared against a specification under identical conditions - and with a modest regulator and a beaker you can hold filter quality firmly in your own hands. For manufacturers, putting a bubble point number on every batch record is the most credible quality statement a sintered element can carry.